

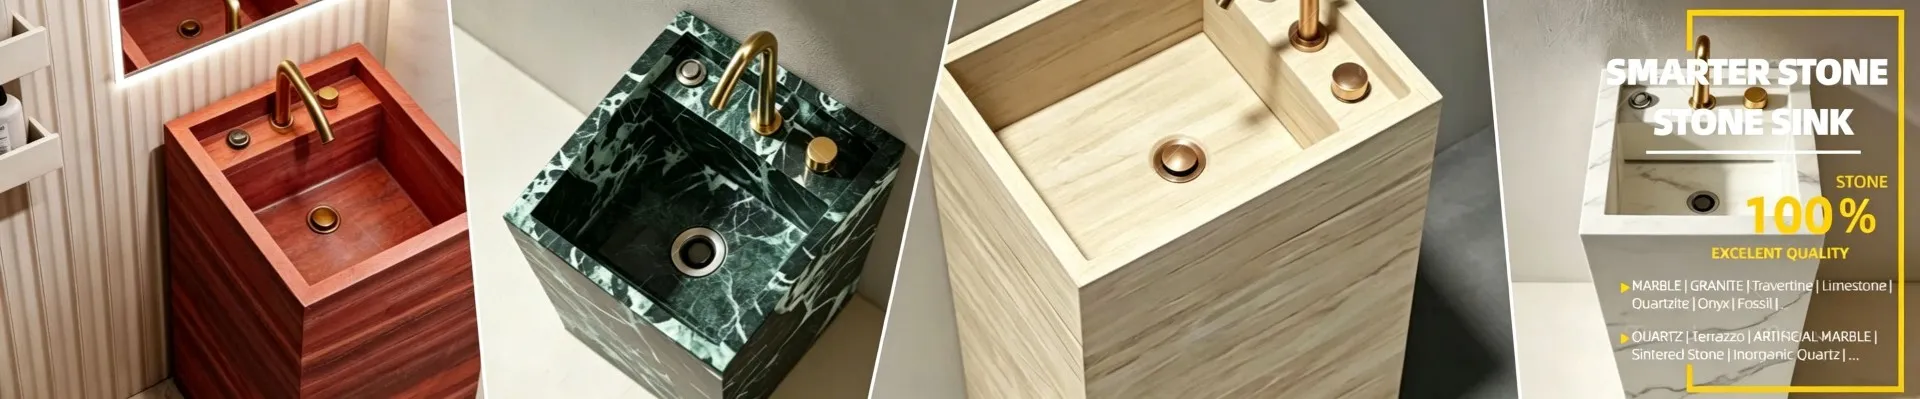
Sintered Stone Wall Panels Wholesale
Sep 29, 2026
Leave a message
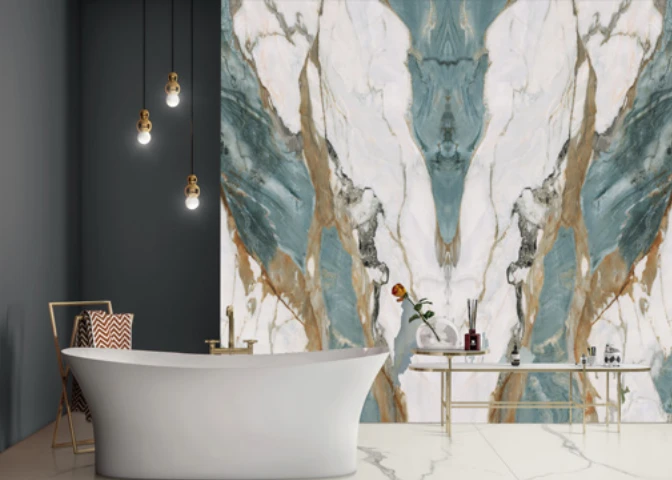
Technical Performance: Sintered Stone vs. Traditional Wall Finishes
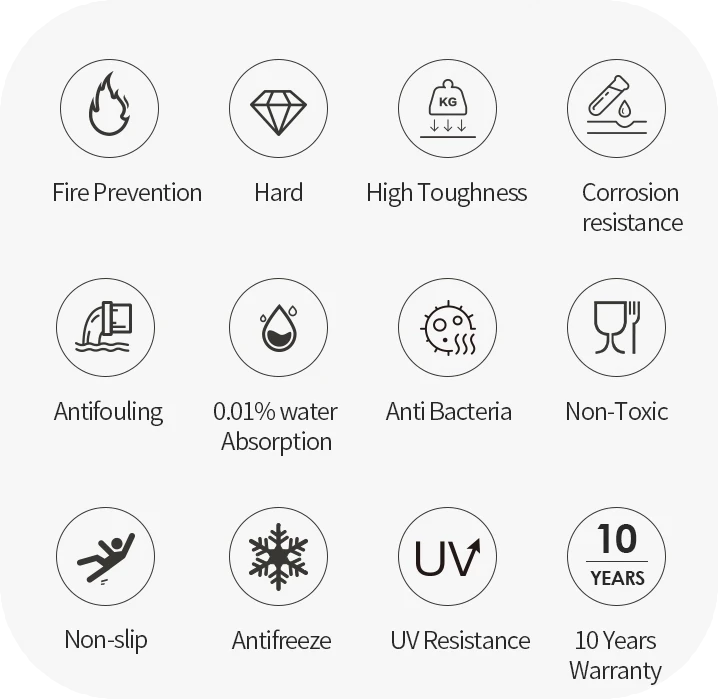
Evaluating interior wall cladding materials requires strict adherence to physical and chemical testing parameters. Large-scale commercial projects and wholesale distribution networks demand predictable material behaviors across moisture absorption, fire propagation, and surface abrasion.
The following material matrix compares 3 mm- 6 mm sintered stone wall panels against conventional wood veneers and natural marble slabs based on standardized ASTM and EN testing benchmarks.
| Performance Metric | 3 mm- 6 mm Sintered Stone Panels | Natural Marble Cladding | Traditional Wood Veneer |
| Water Absorption Rate | $\le 0.05\%$ (ASTM C373) | $0.2\% - 0.5\%$ | $12\% - 15\%$ (Unsealed) |
| Mohs Hardness | Level 7 | Level 3 - Level 4 | Level 1 - Level 2 (Surface coating) |
| Fire Resistance Rating | Class A1 (Non-combustible, EN 13501-1) | Class A1 | Class D / F (Combustible) |
| Flexural Strength | $\ge 45 \, \text{MPa}$ (ISO 10545-4) | $10 - 15 \, \text{MPa}$ | Varies by substrate |
| VOC Emissions | Zero VOC (Inorganic composition) | Zero VOC | Dependent on adhesives/sealants |
| Abrasion Resistance | Deep abrasion $\le 175 \, \text{mm}^3$ | Moderate | Low |
Architectural Applications and Large-Format Logistics
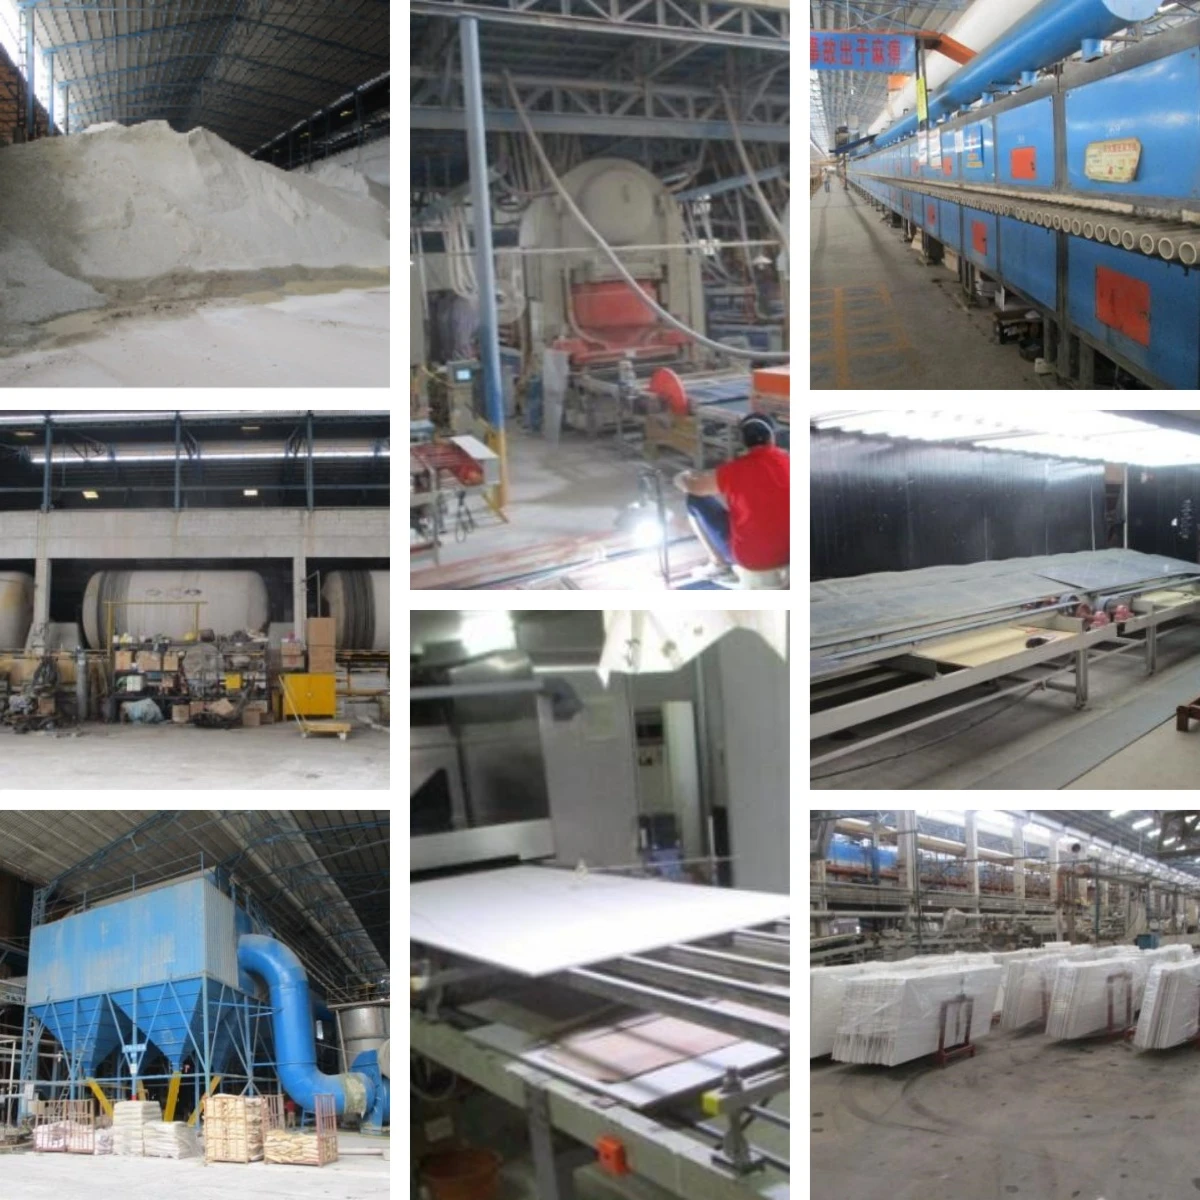
Powerful Solutions For Business Growth
Substrate Compatibility: Panels require rigid backing systems such as marine-grade plywood, cement backer boards, or direct metal stud framing using structural polyurethane or epoxy adhesives compliant with ISO 13007 standards.
Weight Reduction for High-Rises: At 3mm thickness, panels weigh approximately $7.5 \, \text{kg/m}^2$, reducing total dead load on elevator cab interiors, yacht bulkheads, and high-rise commercial corridors compared to standard 20mm stone slabs.
Vein-Matching and Bookmatching: Advanced digital inkjet printing combined with controlled pressing alignment allows continuous vein-matching and bookmatched panel sets for feature walls and elevator lobbies.
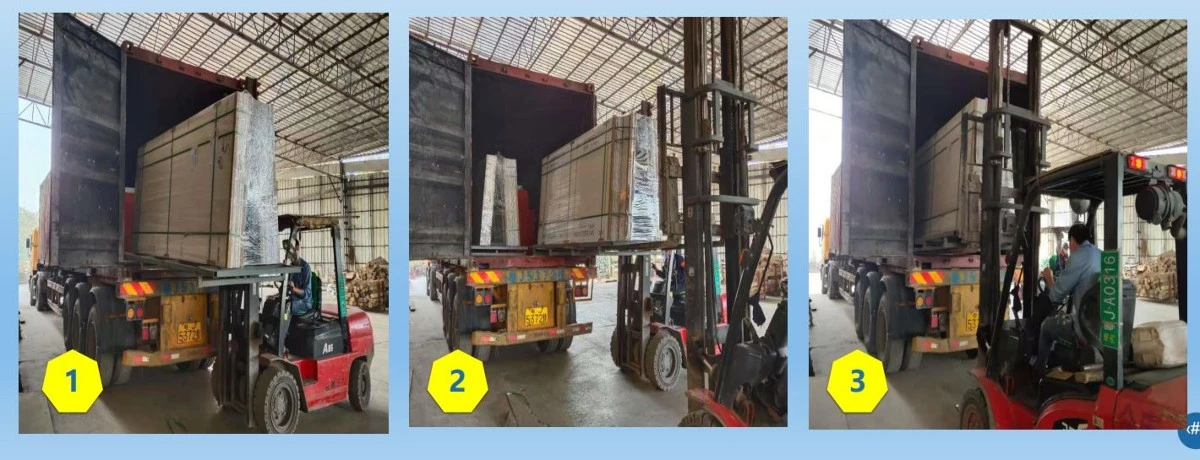
Breakage Rate Control: Wholesale shipments utilize custom A-frame packing inside seaworthy wooden crates, fumigated to ISPM 15 standards, maintaining break-rate control below $0.5\%$ across transoceanic freight.
Sustainable Compliance and Green Building Certification
Environmental product declarations (EPDs) and indoor air quality metrics dictate material selection for LEED, BREEAM, and WELL building standard certifications. Sintered stone manufacturing utilizes natural raw materials-mined quartz, feldspar, and porcelain clays-subjected to a high-pressure compaction process simulating metamorphic rock formation without organic binders or synthetic resins.
Zero-Silica and Low-Crystalline Silica Options: Formulated to meet stringent occupational safety regulations, minimizing airborne respirable dust hazards during fabrication and installation.
Zero VOC Emissions: Emits no volatile organic compounds post-installation, supporting strict indoor air quality requirements for healthcare facilities, educational institutions, and luxury residential developments.
Recyclability: Sintered stone bodies are 100% recyclable at end-of-life, grinding down safely into aggregate materials for secondary construction use.
CE Certification & ASTM Standards: All production batches undergo rigorous third-party testing for frost resistance, chemical resistance, and breaking strength, backed by official CE certification and ASTM standards compliance documentation.
Frequently Asked Questions
What is the maximum installation height for 3mm-6mm sintered stone wall panels without mechanical anchors?
Adhesive-bonded interior wall installations using structural polyurethane generally perform up to 3 meters in height. For heights exceeding 3 meters or public high-traffic zones, combination mechanical clip systems and back mesh reinforcement are recommended to ensure seismic stability and shear resistance.
How does Smarter Stone control color variation across large-batch wholesale orders?
Production utilizes automated spectrophotometer color-monitoring systems during raw material dosing and digital firing cycles. Digital batch mapping ensures that all slabs within a single container shipment fall strictly within Delta E color tolerance parameters ($\Delta E < 0.8$), guaranteeing uniform color continuity across massive commercial wall installations.
What are the standard packaging and damage compensation protocols for wholesale container orders?
All slabs are packed in fumigated A-frame wooden crates secured with steel edge protectors and moisture-barrier films. Smarter Stone maintains a strict breakage rate control threshold below $0.5\%$. In the event of transit damage exceeding the agreed tolerance, photographic evidence submitted within 48 hours of port arrival triggers an immediate replacement or credit note policy.